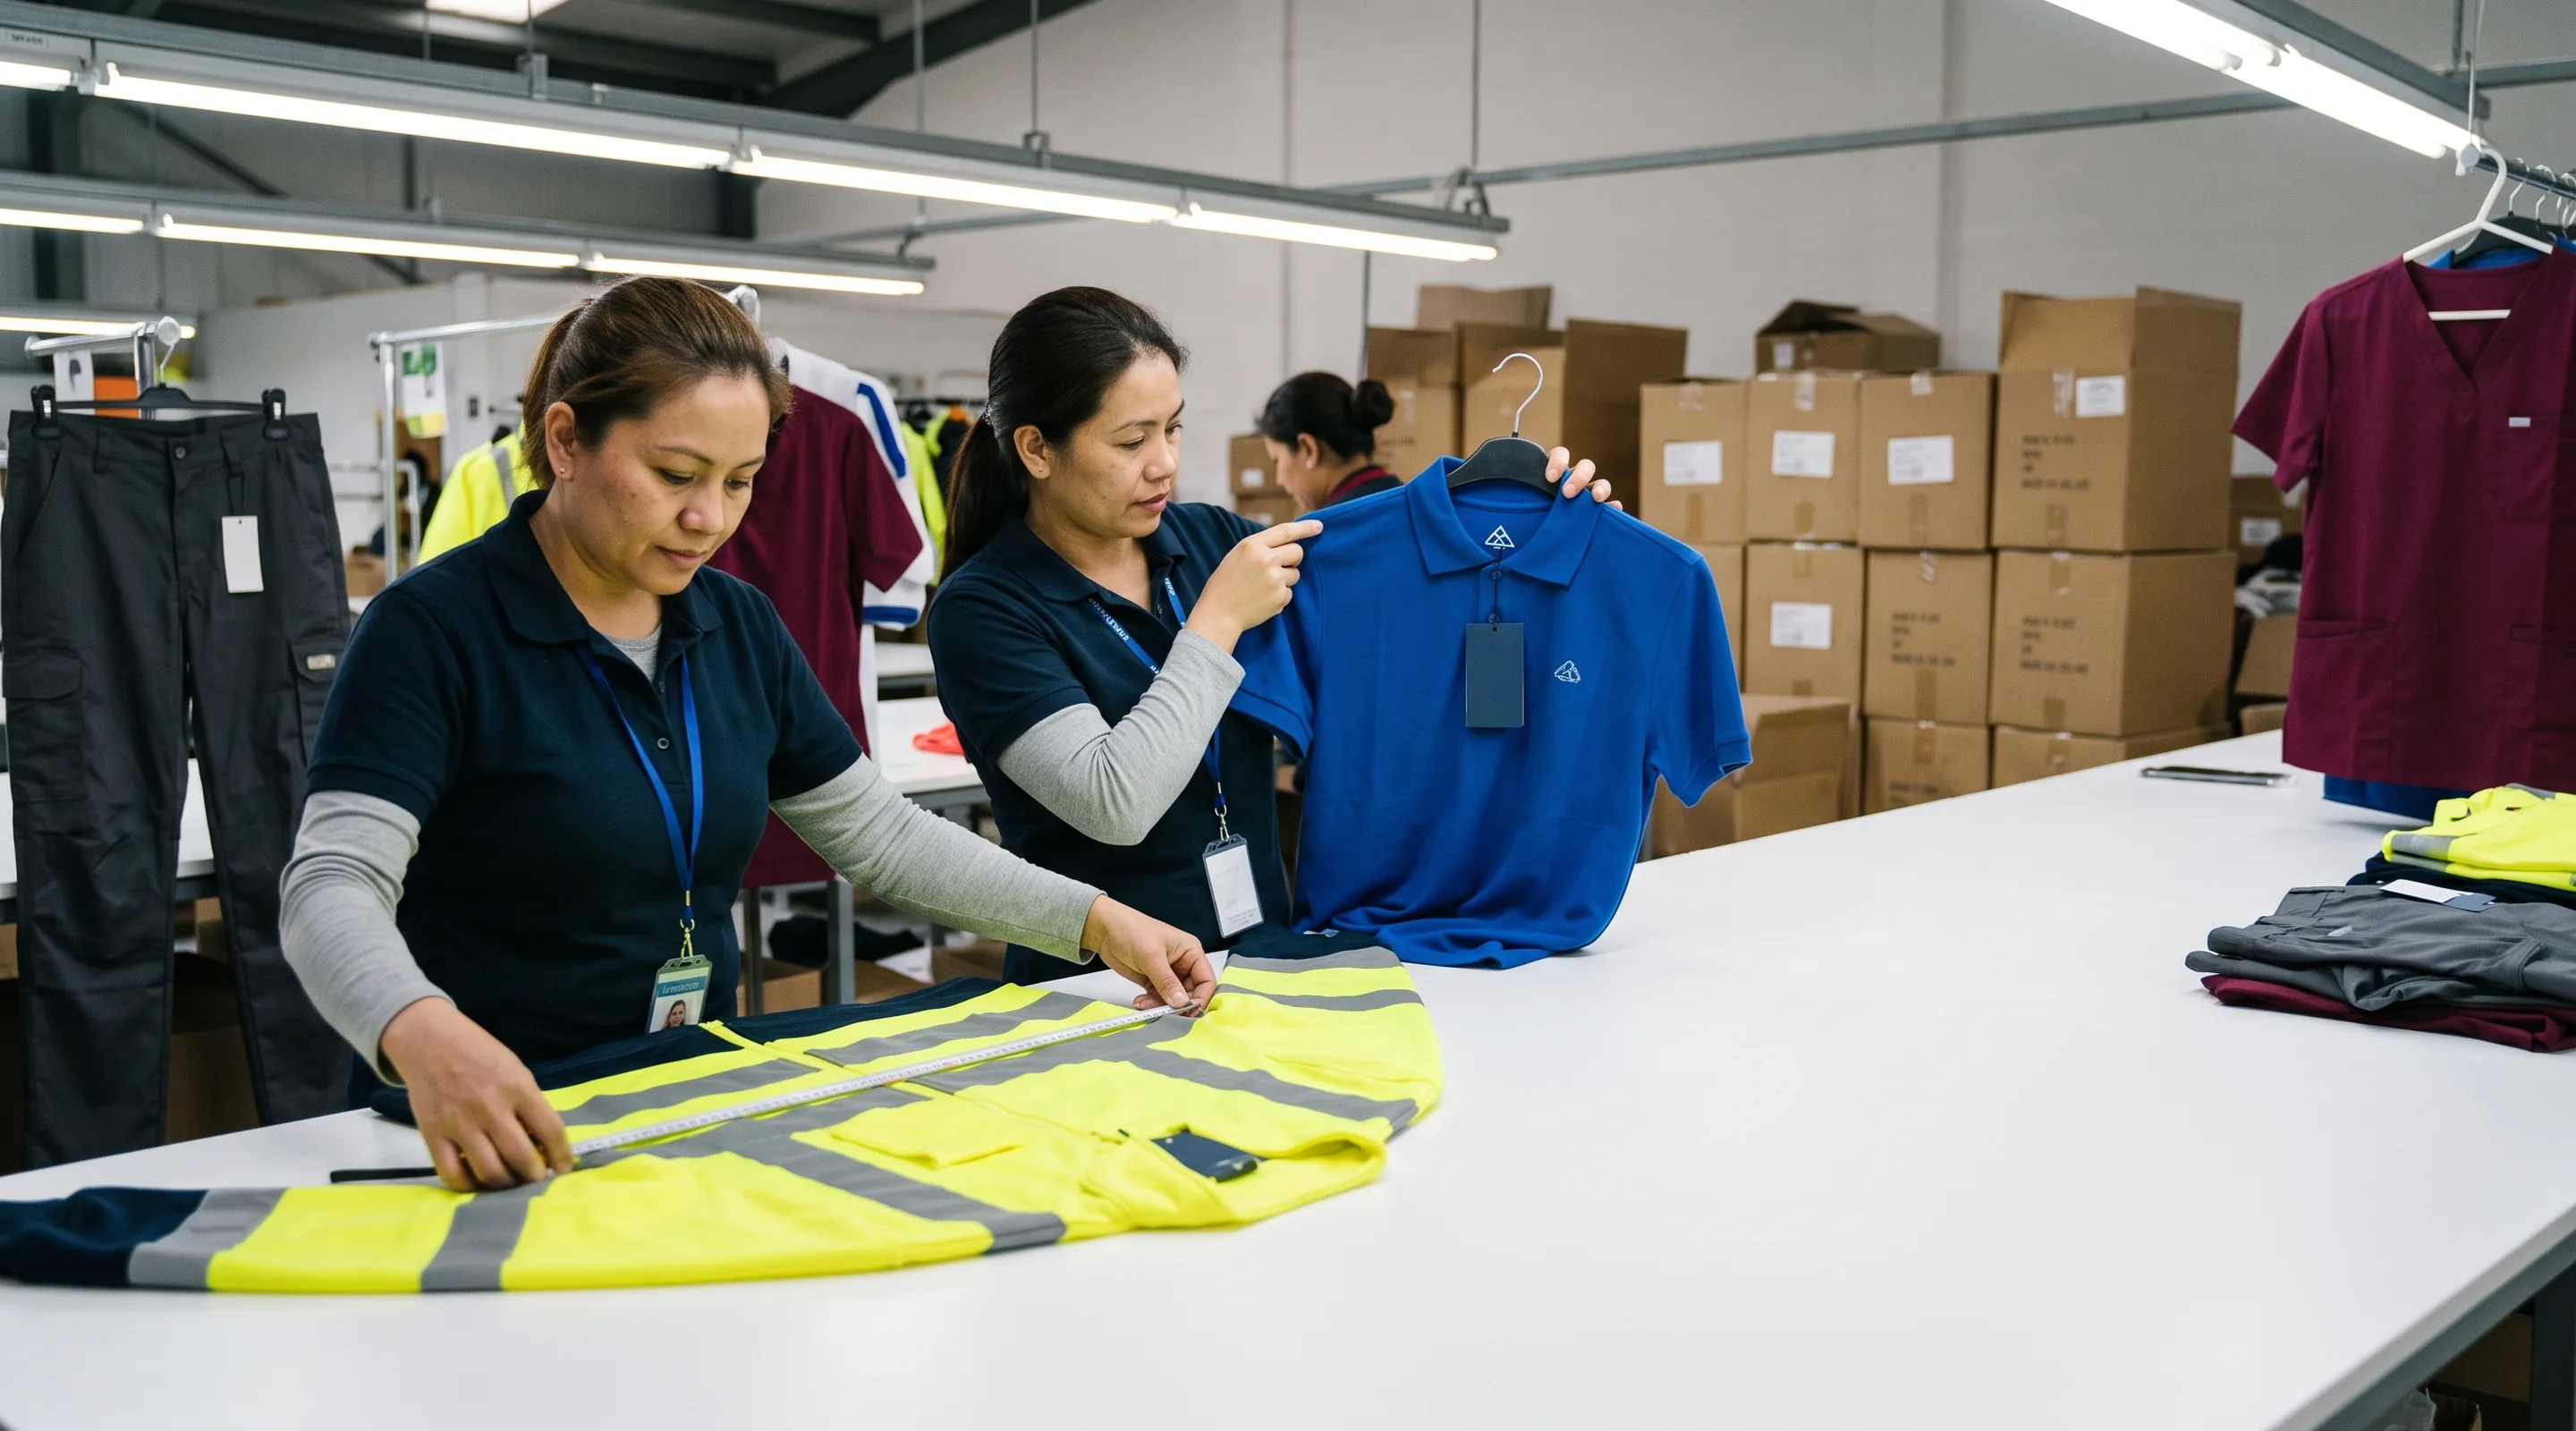
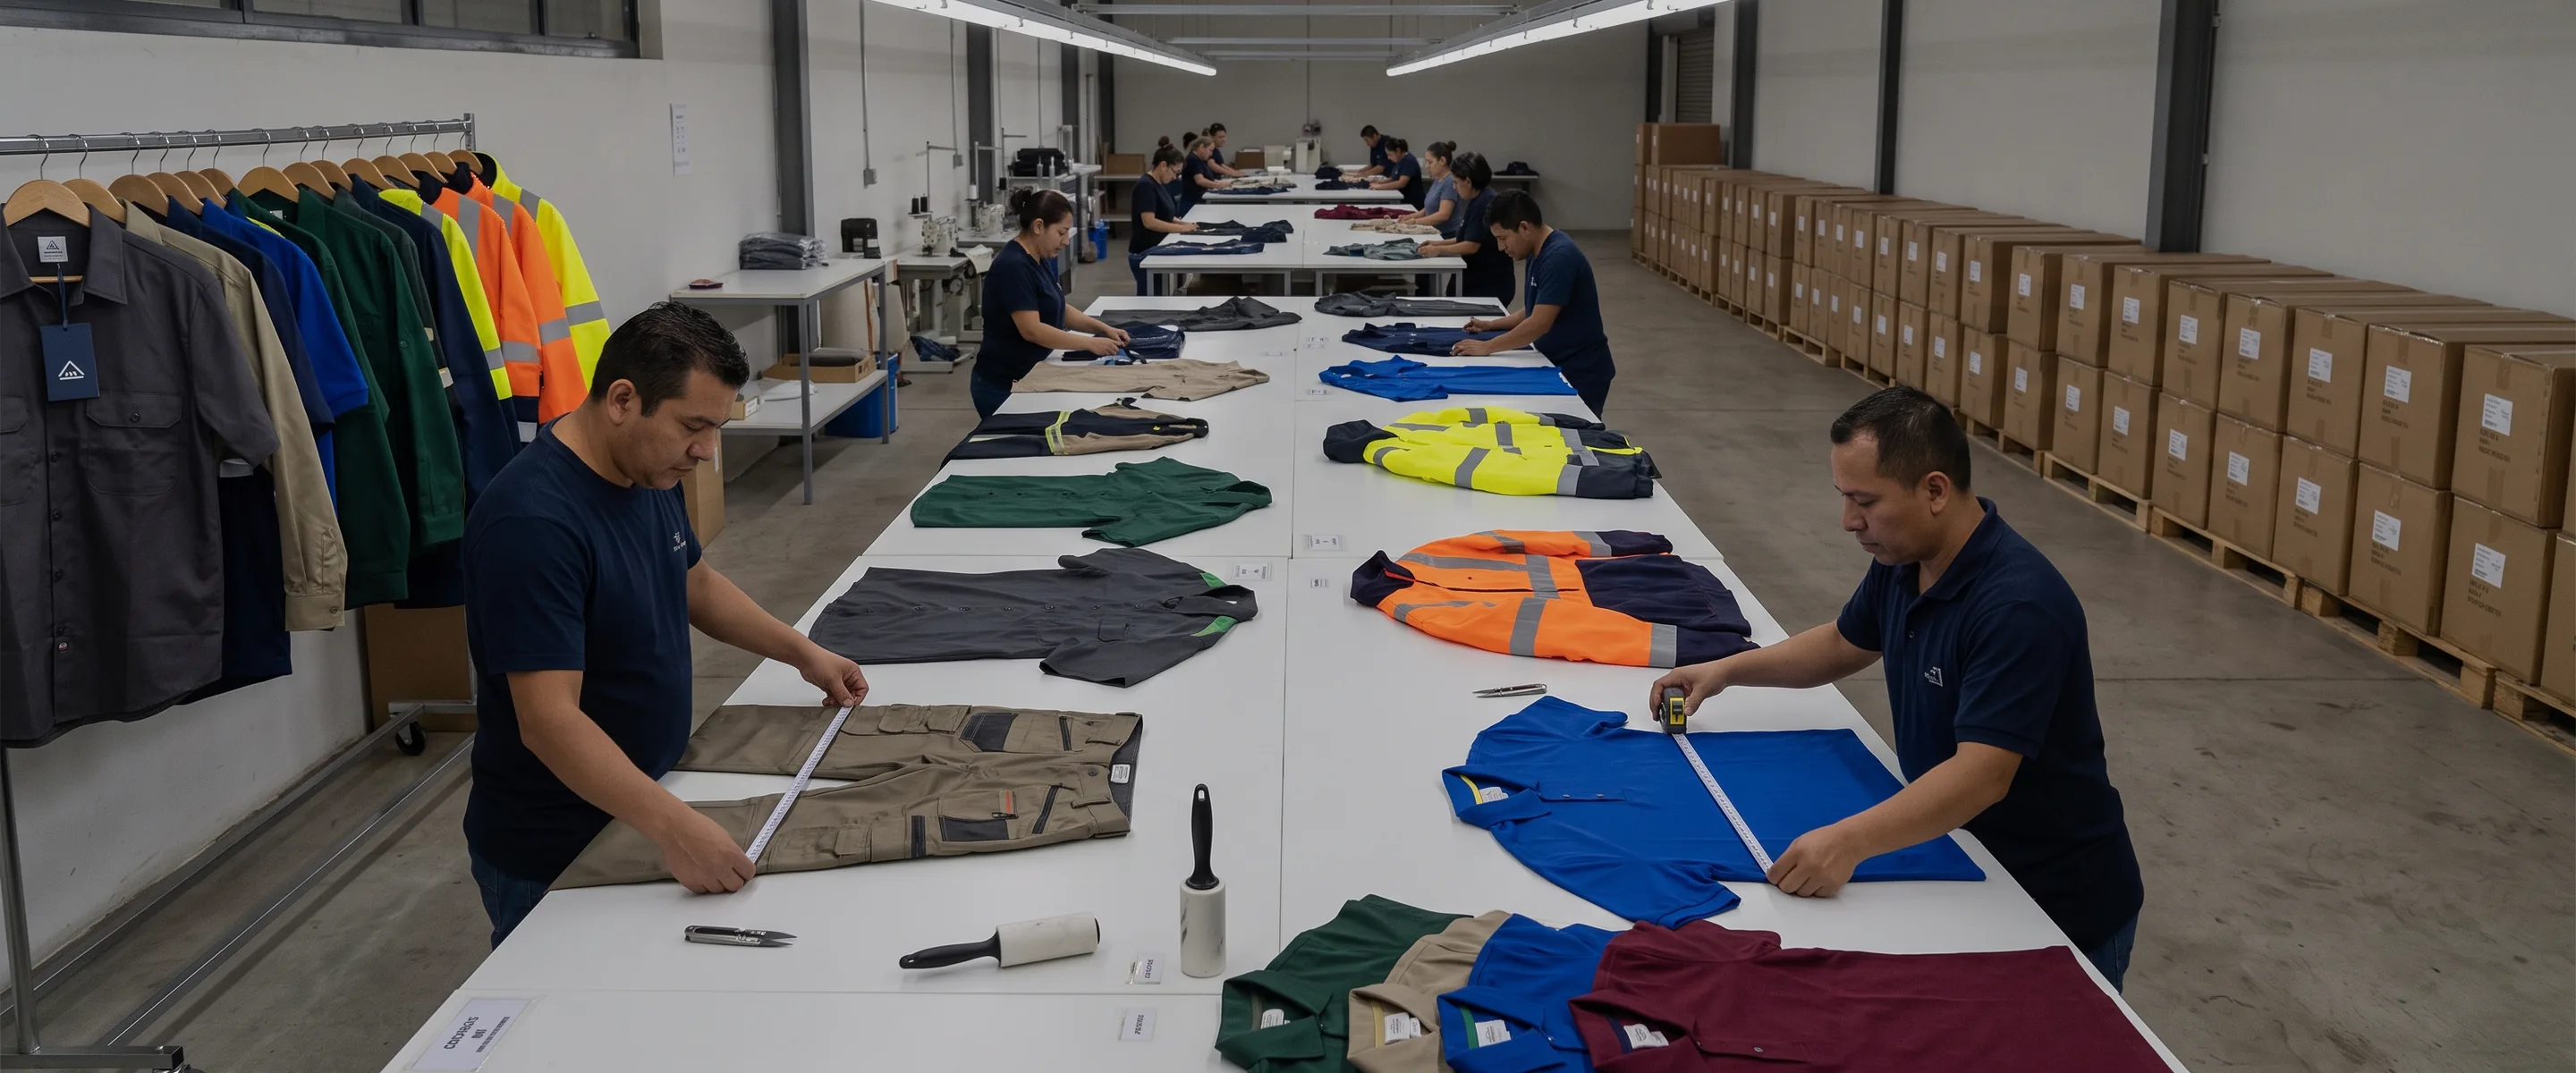
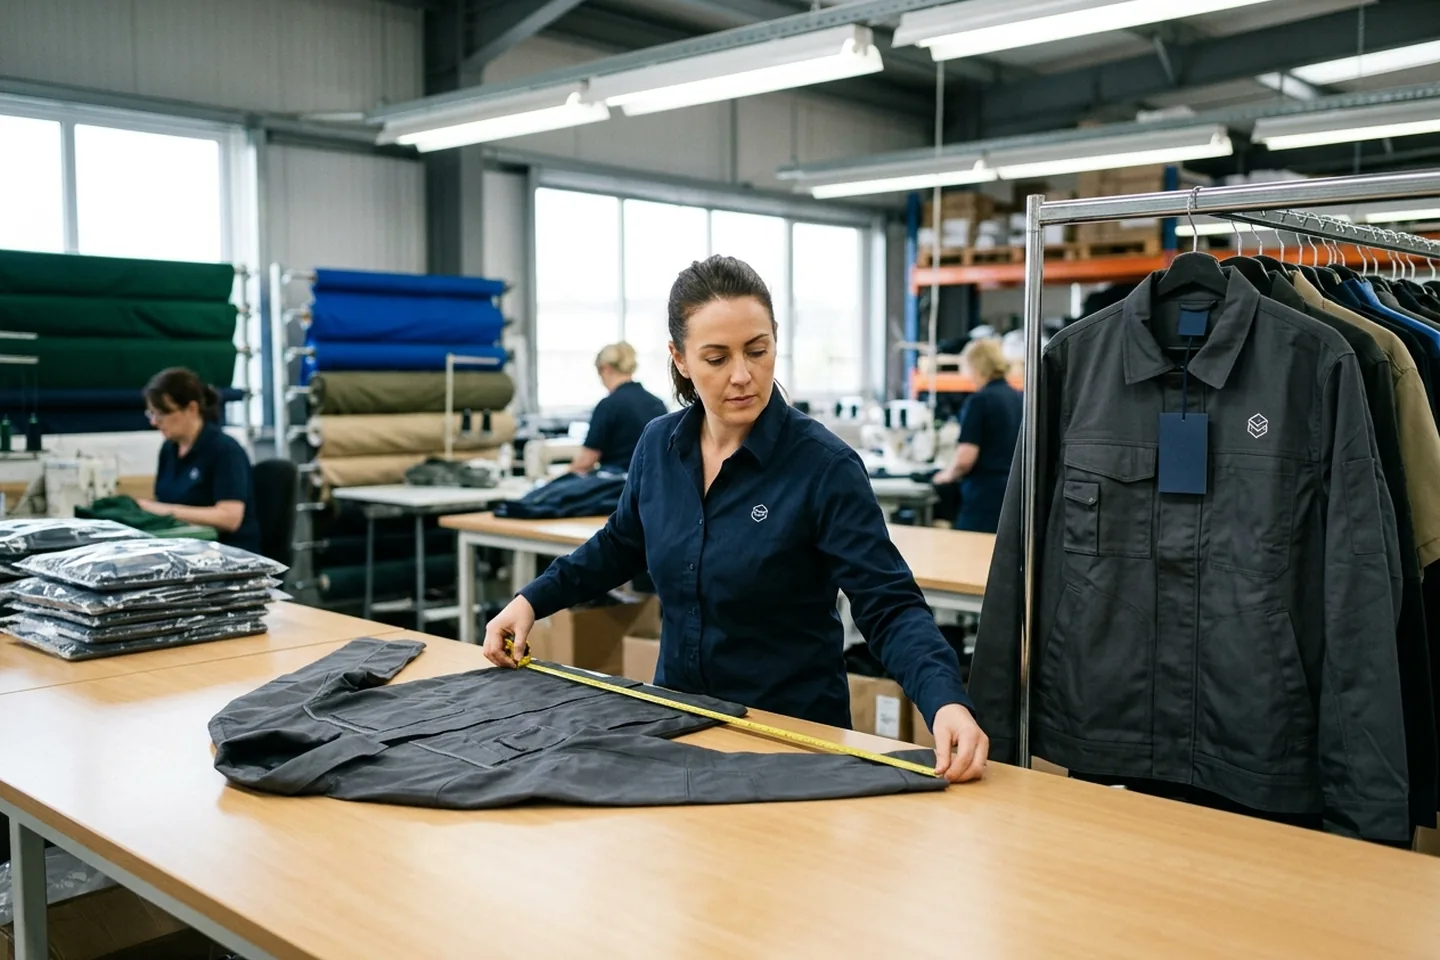
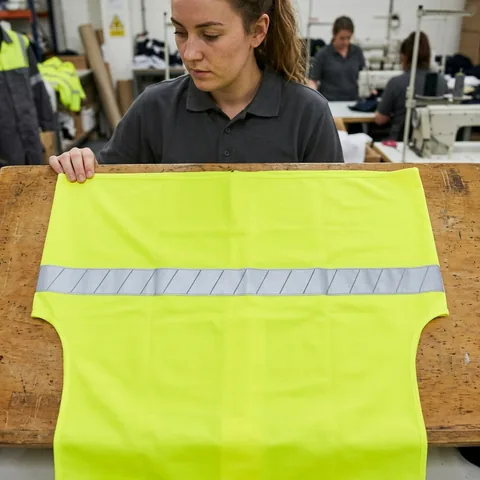
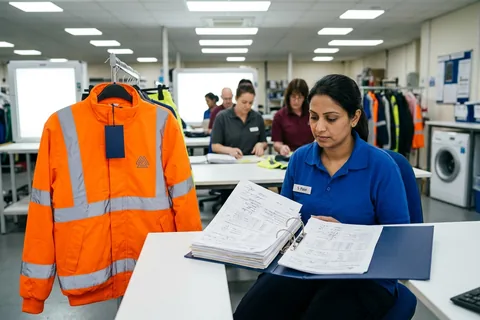
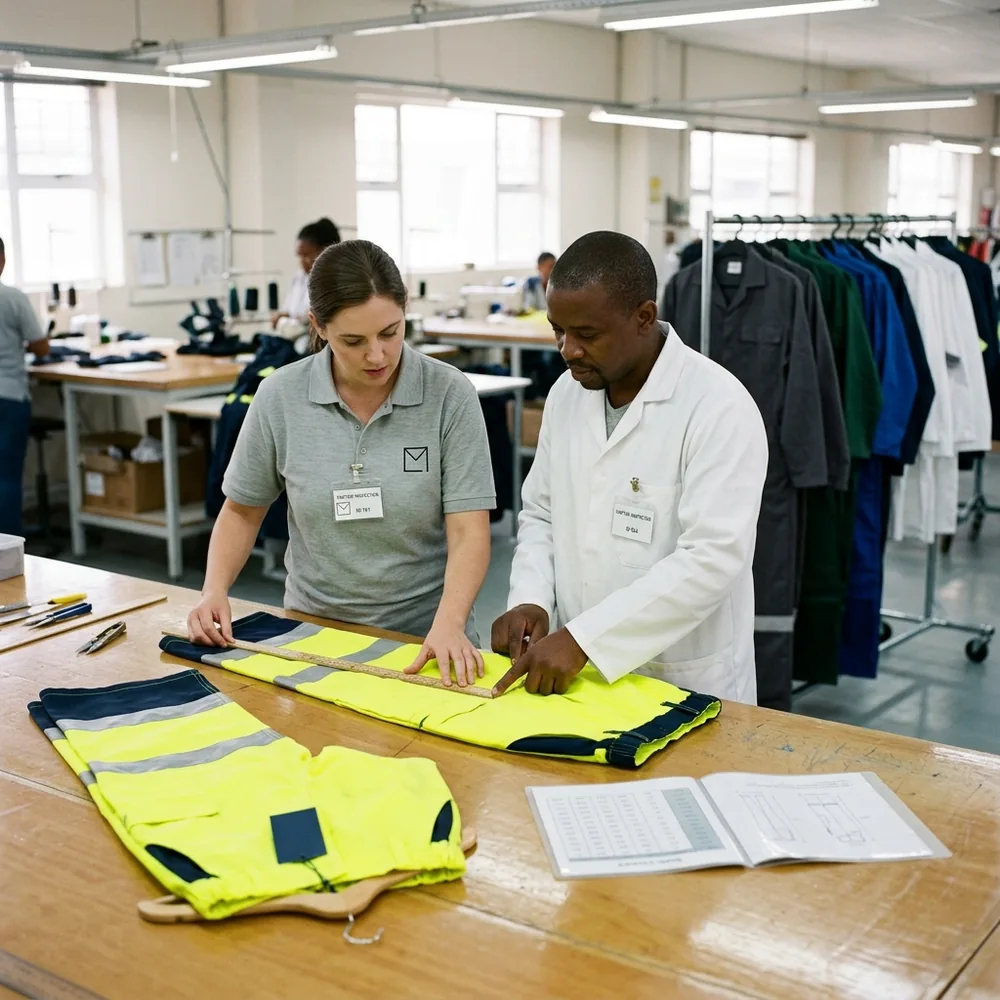
Final inspection room in a uniform factory: one inspector measures a hi-vis jacket laid flat while another compares a polo with the approved sample on a hanger
Workwear factory quality control

Workwear Factory Quality Control, Checked Against Your Approved Sample

A cut-and-sew uniform and workwear factory with in-house embroidery, printing, heat transfer and reflective tape, so every check on your garments is made in one factory, against the sample you approved.
Written for procurement, EHS and brand QA teams approving a supplier.
ISO 9001 quality system covering how our orders are specified, signed off, inspected and recorded.
01Quality system

Uniform Quality Control System: Seven Gates From Approved Sample to Release

Every check is made against one reference: the sample you approved and its signed build spec sheet. How deviations escalate is on our about page.
Your build
The gates stay the same; the checks inside them change.
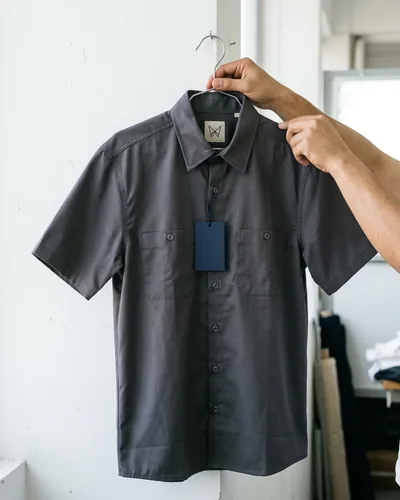
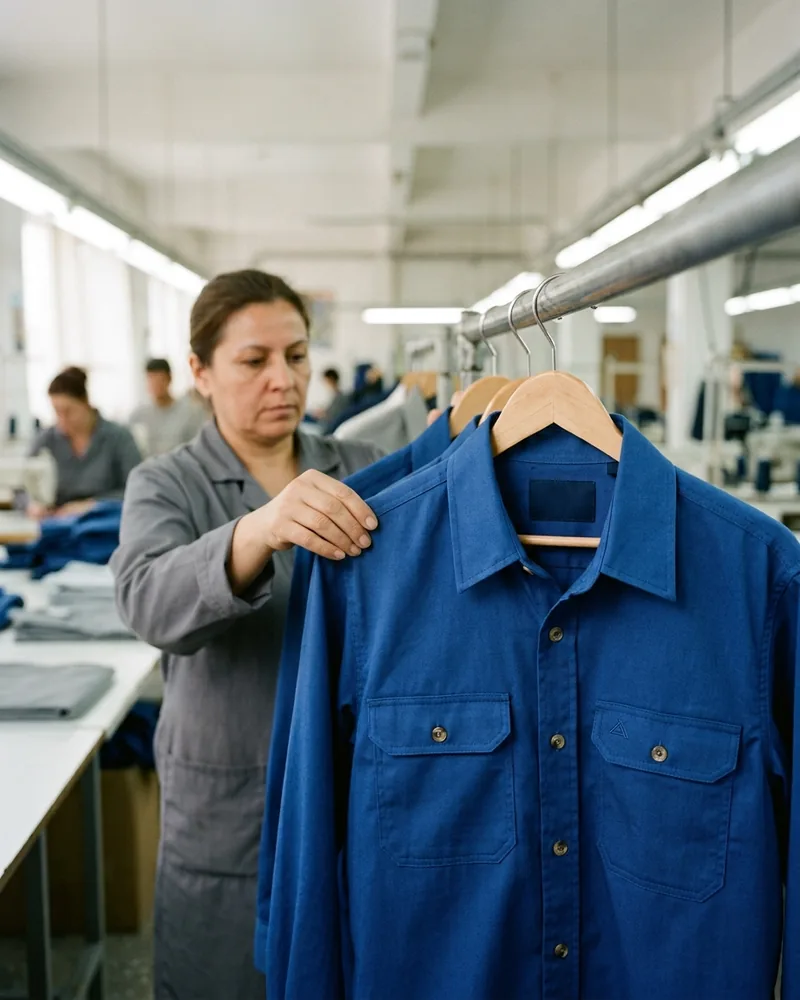
An approved sample work shirt on a hanger with a plain navy swing tag
Reference · your approved sample + signed build spec sheet
  1. 01

    Fabric and trims in

    Incoming inspectors
    Rolls graded, trims checked, shade read before cutting. Gate 01
    Hi-visTape lot logged with the mill's test report
    FRFR trims checked against the signed FR BOM, stored apart
  2. 02

    Pattern approval

    Pattern room lead
    Pattern and grading approved against your sample before any cutting.
  3. 03

    Cut panels

    Cutting-room QC
    Panels checked before they reach a sewing line. Inline point 1
  4. 04

    Line check

    Line QC
    First piece signed on every line, machine and press, then roving rounds. Inline point 2
    Hi-visTape position and bonding on every round
    FRLine-clearance check signed before the order starts
  5. 05

    End of line

    End-of-line checkers
    Every garment checked before pressing and packing. Inline point 3
    NamedEach name against your signed spelling proof
  6. 06

    Final inspection

    Final inspectors
    Packed order sampled and inspected; the QC manager signs the release against the report. Gate 06
    Hi-visA missing or covered band is a critical defect
    FRA non-FR component is a critical defect
    NamedPer-person packs checked against the staff list
  7. 07

    Records and report

    QC manager
    Records filed with your program; the report reaches you before goods leave. Gate 07
02QC team

Seven QC Roles, Each Working at Its Own Station

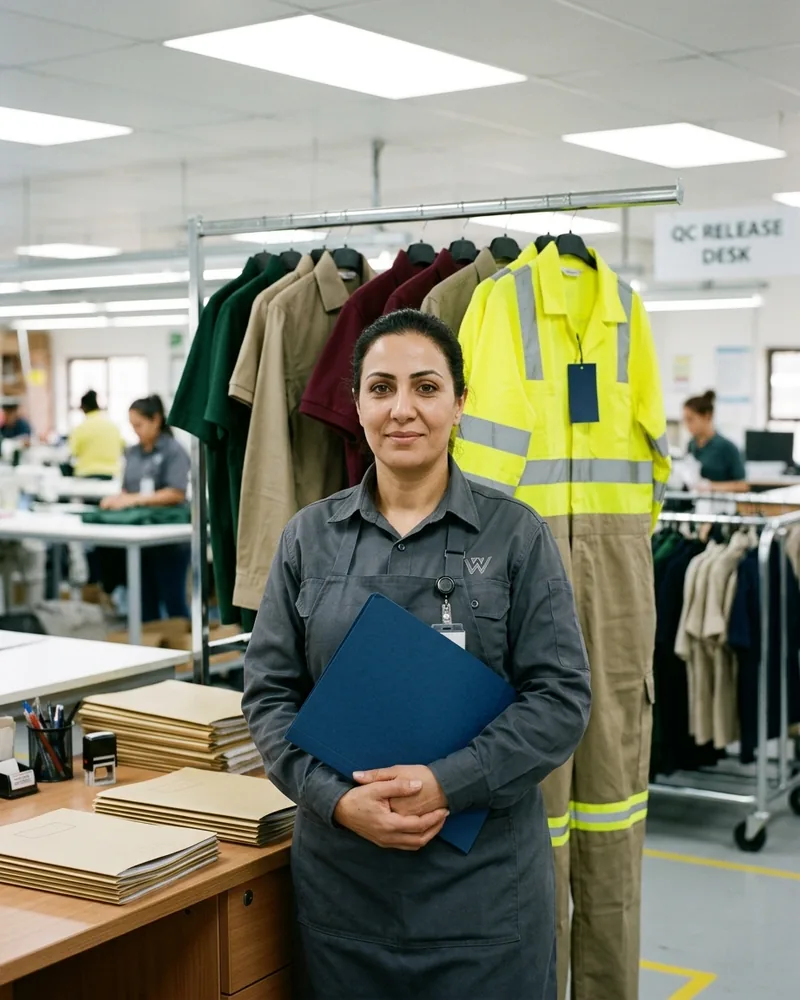
The QC manager at the release desk holding a report folder, approved samples hanging behind
Release desk

QC manager

  • Sets the inspection standard at sample approval
  • Decides on every deviation
  • Signs the final release against the written report
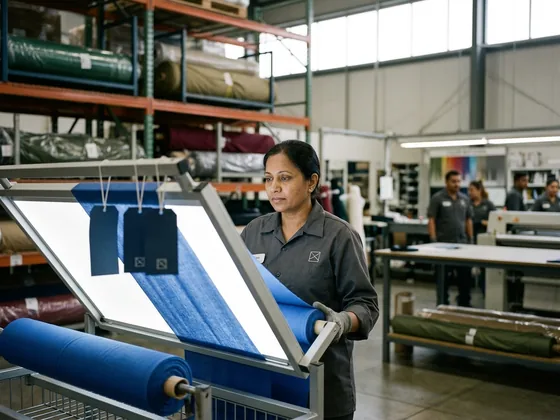
An incoming inspector running a fabric roll over a lit inspection frame
Fabric store

Incoming inspectors

Rolls on a lit frame, width and gsm, and every trim lot against the order.
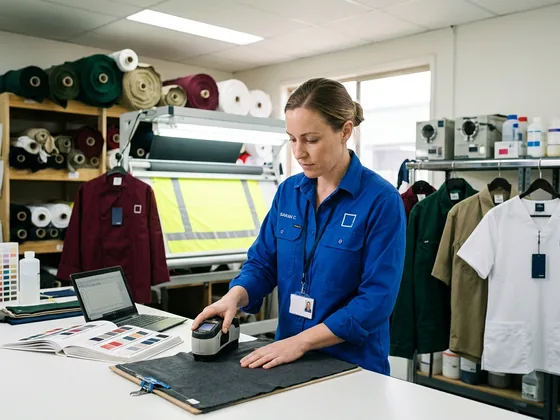
A colour lab technician pressing a spectrophotometer onto fabric
Colour lab

Colour lab technician

Reads each fabric batch against the retained lab dip before it is released to cutting.
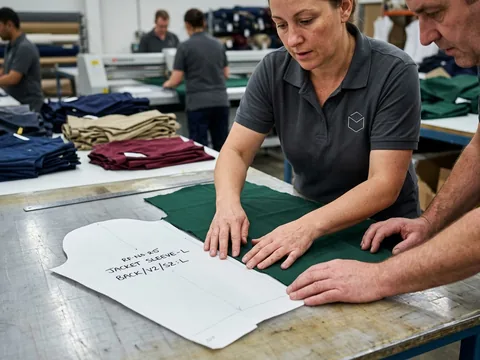
Cutting-room QC laying cut panels against the paper pattern
Cutting room

Cutting-room QC

Checks panels and bundles before they leave for the sewing lines.
Line QC checking a freshly sewn garment beside a sewing line
Sewing lines

Line QC

One per sewing line. Signs the first piece, then roves that line.
An end-of-line checker turning over a finished work jacket
End of line

End-of-line checkers

Handle every finished garment and take the daily measurements.
A final inspector drawing garments from a sealed carton
Final inspection room

Final inspectors

Draw the sample from the packed order and inspect it against the approved sample.
Your program's role holders are named on the contact sheet sent with the sample plan, as set out on our about page.
03Incoming fabric

Incoming Fabric: 4-Point Grading on at Least 10% of Each Dye Lot

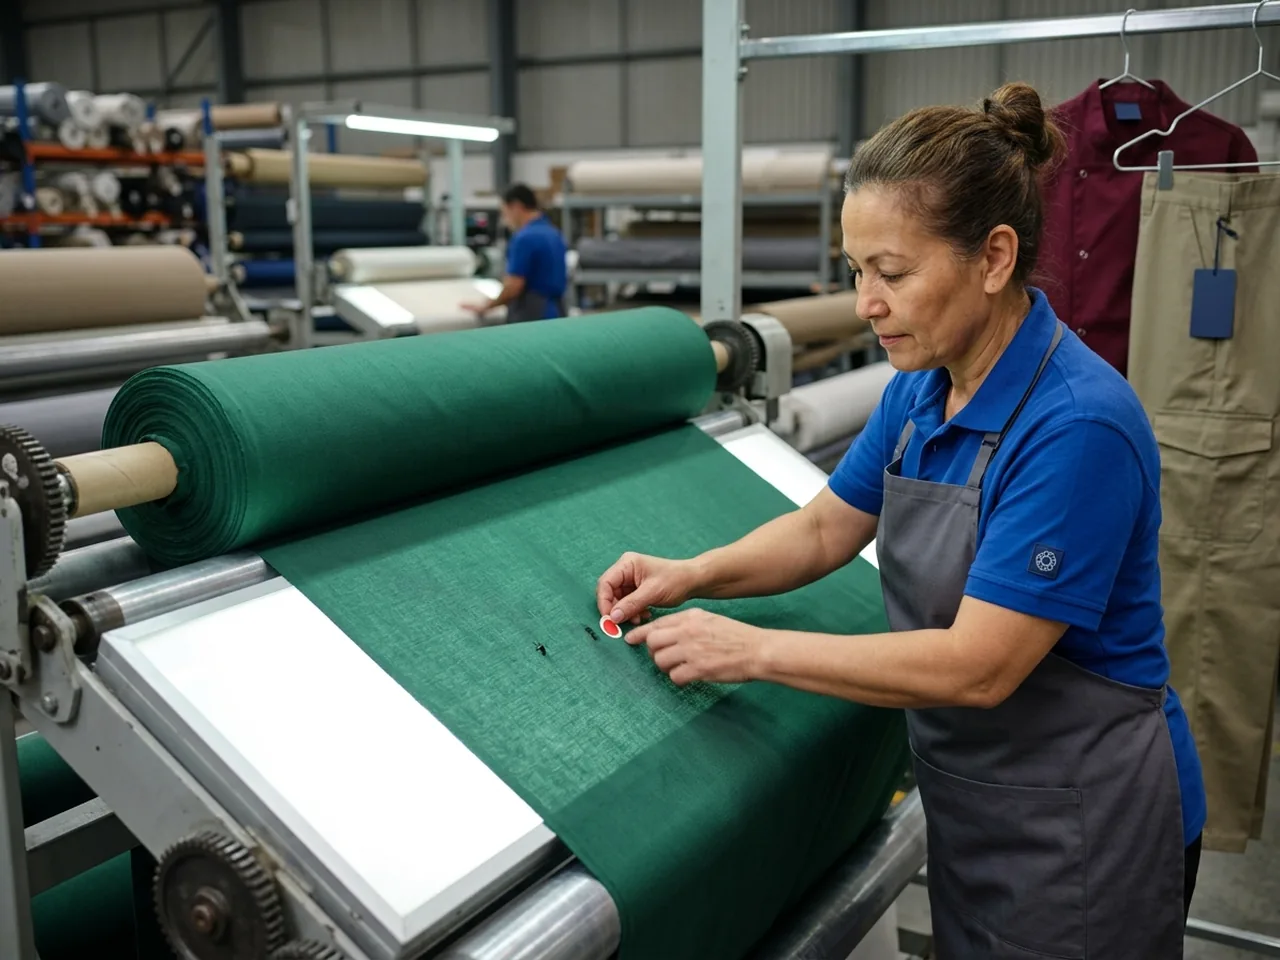
Fabric is inspected before it is accepted into the fabric store, so a faulty roll is stopped before it is cut into panels.
A fabric roll running over a lit inspection frame while an inspector marks a fault with a small sticker
1 pointFault up to 3 in
2 pointsOver 3 to 6 in
3 pointsOver 6 to 9 in
4 pointsOver 9 in
Accept
Reject · lot inspection extended
040 points per 100 yd²80
Grading
Every visible fault scored to the 4-point system (ASTM D5430), totalled per 100 yd².
Sampling
At least 10% of the rolls in every dye lot; each one checked for usable width and gsm against your order.
Rejects
A roll over the limit goes back to the mill or is replaced, and more rolls of that lot are inspected.
Shade before cutting
Each batch read against your retained lab dip under D65. Outside tolerance it is held, re-dyed or replaced, and you are told before cutting if the date moves. Colour lab
Lot records
Hi-vis and FR fabric and tape lots are logged with the mill's test report.
Trims
Trim lots of zippers, buttons and thread cones checked on a tableItem, colour and quantity per lot. FR trims are checked against the signed FR BOM and kept in a separate tagged store. FR clothing
The incoming inspector signs the roll sheet for each lot; the colour lab technician signs the shade reading.
04Fabric tests

Fabric and Component Tests Run Before Cutting

Run at lab-dip and fabric stage. Each row links to the full method.
A lab technician recording readings beside a spectrophotometer and a row of fabric swatches
Show tests for
Put these tests in my QC plan
Fabric and component tests run before cutting
TestMethod and pass levelApplies toFull method
Re-order shadeSpectrophotometer against your retained lab dip, ΔE ≤ 1.0, read before cuttingEvery colourColour lab
Cross-fabric colour matchΔE2000 ≤ 2.0 to the Pantone target, viewed under D65 and illuminant AHotel and whole-shop mechanic programsHotel uniforms
Hypochlorite fastnessISO 105-N01, grade 4 or better, at lab-dip stageScrubs, coloured chef coats, housekeepingScrubs
Peroxide fastnessISO 105-N02, grade 4 or better, at lab-dip stageSalon apronsAprons
Shrinkage after launderingISO 5077, 3% or lessScrubs, chef coats, mechanic garments, housekeepingScrubs
Oily stain releaseAATCC TM130, grade 3.5 new and 3.0 after ISO 15797 × 25Mechanic garments with soil-release finishMechanic uniforms
AbrasionMartindale ISO 12947-2: 40,000 rubs rigid twill, 30,000 stretch, 80,000 knee overlayWork pantsWork pants
Seam strengthISO 13935-2, crotch seam 250 N or moreWork pantsWork pants
Stretch and growthASTM D3107, growth 5% or lessStretch work pantsWork pants
Water-resistant coatingISO 811, 1,000 mm new and 600 mm after ISO 6330 × 25Coated salon and prep apronsAprons
FR component checkEvery thread, trim and label checked against its FR report or supplier declaration, on the signed FR BOMFR shirts, pants, coveralls, FR hi-visFR clothing
Hi-vis and FR fabric and tapeThe mill's test report for each lot, recorded against the orderHi-vis and FR buildsSafety vests
Fabric roll inspection4-point grading, width and gsm, to the limit aboveEvery fabricIncoming fabric
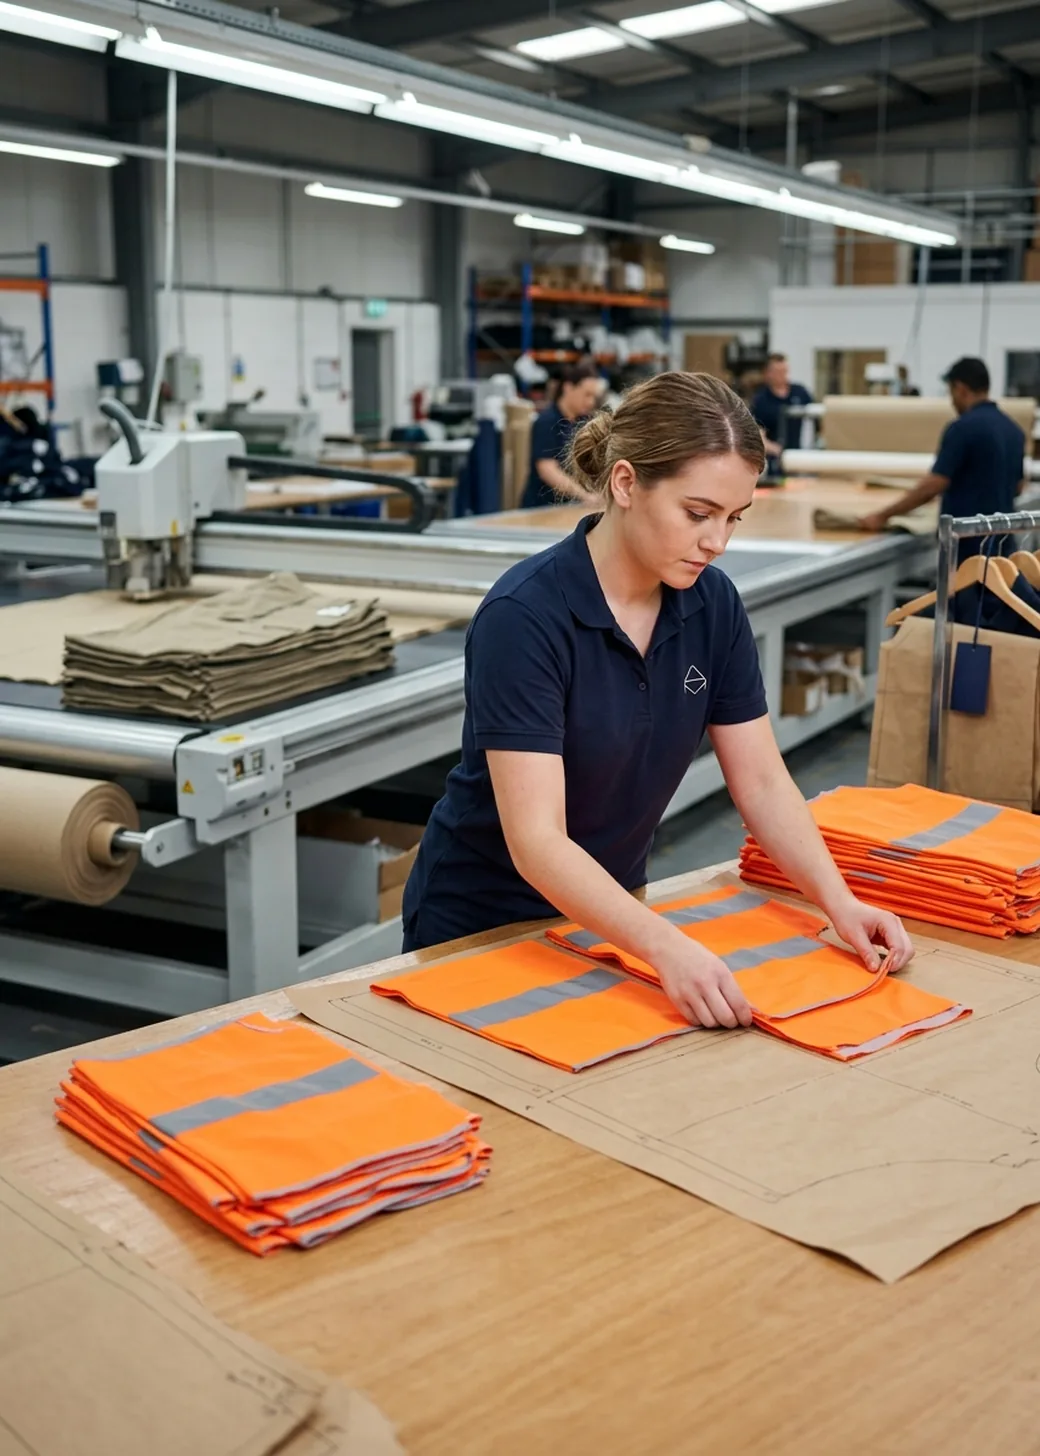
Cutting-room QC laying cut panels on the approved pattern beside an automatic multi-ply cutting table
05Inline QC point 1

Inline QC Point 1: Cut Panels Checked Before Sewing

Panels are cut from your style's CAD marker file on our 2 automatic multi-ply cutting tables, and the same file cuts every re-order.
A cut panel edge lined up against the paper pattern

Shape against the pattern

Panels from the top, middle and bottom of each lay go on the approved pattern. A shifted lay stops and is re-checked against the file.
A stack of cut panels tied with a bundle ticket

One dye lot per bundle

Right panel count, one dye lot, a ticket with style, size, colour and dye lot that follows it to your carton.
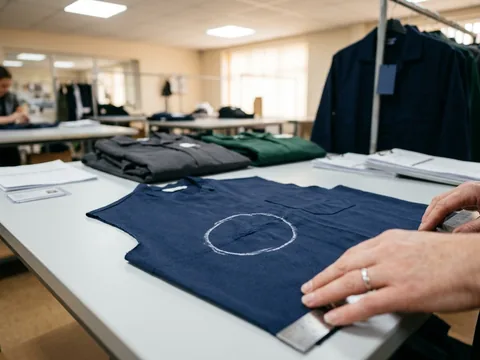
A weaving fault circled in chalk on a cut panel

Faults and marks

Notches and drill marks in place. A panel with a fault, stain or shading is pulled and recut from the same dye lot.
Recorded: a signed cut-panel check sheet for each lay. Panels embroidered before assembly are checked at point 2.
06Inline QC point 2

Inline QC Point 2: Signed First Piece, Roving Checks Every 2 Hours

The first finished shirt off a line, on a hanger with a plain navy tagFirst piece · signed
  • On every sewing line, embroidery machine and heat press, against the approved sample and build spec sheet
  • On hi-vis, a new size gets a new first piece
Line QC roves each sewing line every 2 hours and pulls 5 pieces from each operation.
Round 12 h2 h2 h2 h2 h
One line QC per line: the person who signed the first piece roves that line through the run.
  • Stitch type, density and seam allowance
  • Bartacks and seam-strength points
  • Collars, plackets and pockets
  • Zippers, snaps and buttons
  • Reflective tape position and bonding on hi-vis
  • Logo position and finish
  • Labels in place and correct
Line QC pulling a piece from a sewing operator to check it against the approved sample

One faulty piece

The operator corrects the operation, and the next round re-checks it.

A repeat or set-up fault

The line stops and goes to the QC manager within the same shift; a hi-vis press gets a new first piece.

Spec or ship date affected

You are told, as set out under held goods.
Before an FR order, line QC signs the line-clearance check. FR clothingAsk for the QC plan for your program
07Inline QC point 3

Inline QC Point 3: Every Garment Checked Before Pressing and Packing

End-of-line checkers handle 100% of pieces after sewing and decoration, visually and by function.
01

Seams

No open seams, skipped stitches or puckering.
02

Closures

Zippers run, snaps and buttons hold, breakaway points open and re-close.
03

Decoration

Logo present and in position; no broken stitches, cracking or lifted edges.
04

Names

Each name against the spelling proof you signed. A mismatch is a defect.
05

Labels

Size label matches; care, compliance and own-brand labels in place.
06

Finish

Loose threads trimmed, no stains or marks.
Measured daily: 3 pieces per style, colour and size, to the tolerance for that garment (garment tests). A size out of tolerance is traced back by line QC before it continues. Pack-by-person: checked garments matched to the staff list before packing. A failed piece gets a hold tag and goes back for repair or remake (held goods).
An end-of-line checker running the zipper of a hi-vis jacket, a stack of garments waiting beside her
Nothing is packed until a checker has handled it; nothing ships until the QC manager signs.
One reference · seven gates
08AQL sample sizes

AQL Sample Sizes: ISO 2859-1, General Inspection Level II

Garment inspection to AQL follows ISO 2859-1 / ANSI/ASQ Z1.4, single sampling, normal inspection. Each style and colour on your order is one lot.
Find your lot size in the table.
AQL sample sizes and accept / reject numbers by lot size, General Inspection Level II
Lot size (pieces)281–500501–1,2001,201–3,2003,201–10,00010,001–35,000
Sample size5080125200315
Major: accept / reject3 / 45 / 67 / 810 / 1114 / 15
Minor: accept / reject5 / 67 / 810 / 1114 / 1521 / 22
CriticalNone accepted at any lot size
A final inspector drawing pieces at random from several opened cartons of one lotPieces are drawn at random from across the packed lot, not from the top carton. Defect classes and what is checked on each piece: final inspection.
09Final inspection

Final Inspection: Zero Critical, AQL 2.5 Major, AQL 4.0 Minor

Every order is released on a final inspection in the final inspection room, signed by the QC manager. Pieces are drawn at random across the packed lot to the sampling plan.
Critical0accepted
A non-FR component on an FR build, a missing or covered reflective band, a missing compliance label.
Major2.5AQL
An open seam, a failed closure, a size out of tolerance, a logo out of position, wrong thread or ink, broken stitches or lifted decoration, a name unlike the proof, a wrong label.
Minor4.0AQL
An untrimmed thread end, a small mark that cleans off.
A final inspector measuring a work jacket on a long table, the approved sample hanging beside her

Checked on every sampled piece

  1. ShadeAgainst the approved sample and retained lab dip
  2. MeasurementsTo the size spec and tolerance
  3. WorkmanshipSeams, bartacks, pockets, collars
  4. FunctionZippers, snaps, buttons, breakaways, hoods
  5. DecorationAgainst the logo set-up record
  6. NamesAgainst the signed spelling proof
  7. LabelsBrand, size, care and compliance
  8. PackingPolybag, size sticker, per-person packs
  9. CartonsCount, PO, style, colour, dye lot

When a lot fails

Not released: sorted piece by piece, defects repaired or replaced, re-inspected to the same plan. One critical defect rejects the lot.

The release

The QC manager reviews the report and signs. Industrially laundered programs also need the passed pre-production wash tests. Nothing ships before that signature.

The report

Lot and sample size, accept and reject numbers, defects by class, measurements, photos and signature, sent before goods leave.
Need a tighter AQL? Tell us at quote stage.Ask for a sample final inspection report
10Held goods

Nonconforming Product: Hold Tag, Quarantine, Then Repair or Remake

Any garment, panel or lot that fails a check is physically separated, so it cannot be packed by mistake.

Hold

Tagged where it was found: cutting room, sewing line, end of line or final inspection.
01 02

Quarantine

A marked area kept apart from checked goods until a decision is made.
03

Decide

Line QC decides single pieces with a clear repair. Lots, repeats and anything touching the spec go to the QC manager within the same shift.
Tagged garments on a rack inside a taped-off quarantine area

04 · Repair

An operator re-sewing an open seam on a held garment
Only faults that can be corrected without weakening the garment: a seam re-sewn, a closure replaced, threads trimmed. Every repaired piece goes back through the end-of-line check before it can be packed.

04 · Remake

New panels cut from the same dye lot for a remade garment
New cut panels from the same dye lot, through the same checks. Three faults are never repaired:
Hi-vis tape off position or poorly bonded
Heat-applied tape is never peeled and re-pressed: a second press weakens the bond and marks the fluorescent fabric.
A non-FR component on an FR build
The piece is remade from a new cut panel and the lot is checked back.
A logo that will not come out cleanly
Where removal would leave needle holes or marks, the panel is remade.
Your ship date. If a hold affects the spec or the date, your account manager tells you within 24 hours, with what happened and the new date.
Insignia. Rejected security insignia are cut through and logged. Security uniforms
After delivery. Reporting window, response times and remake terms: if a batch is off.

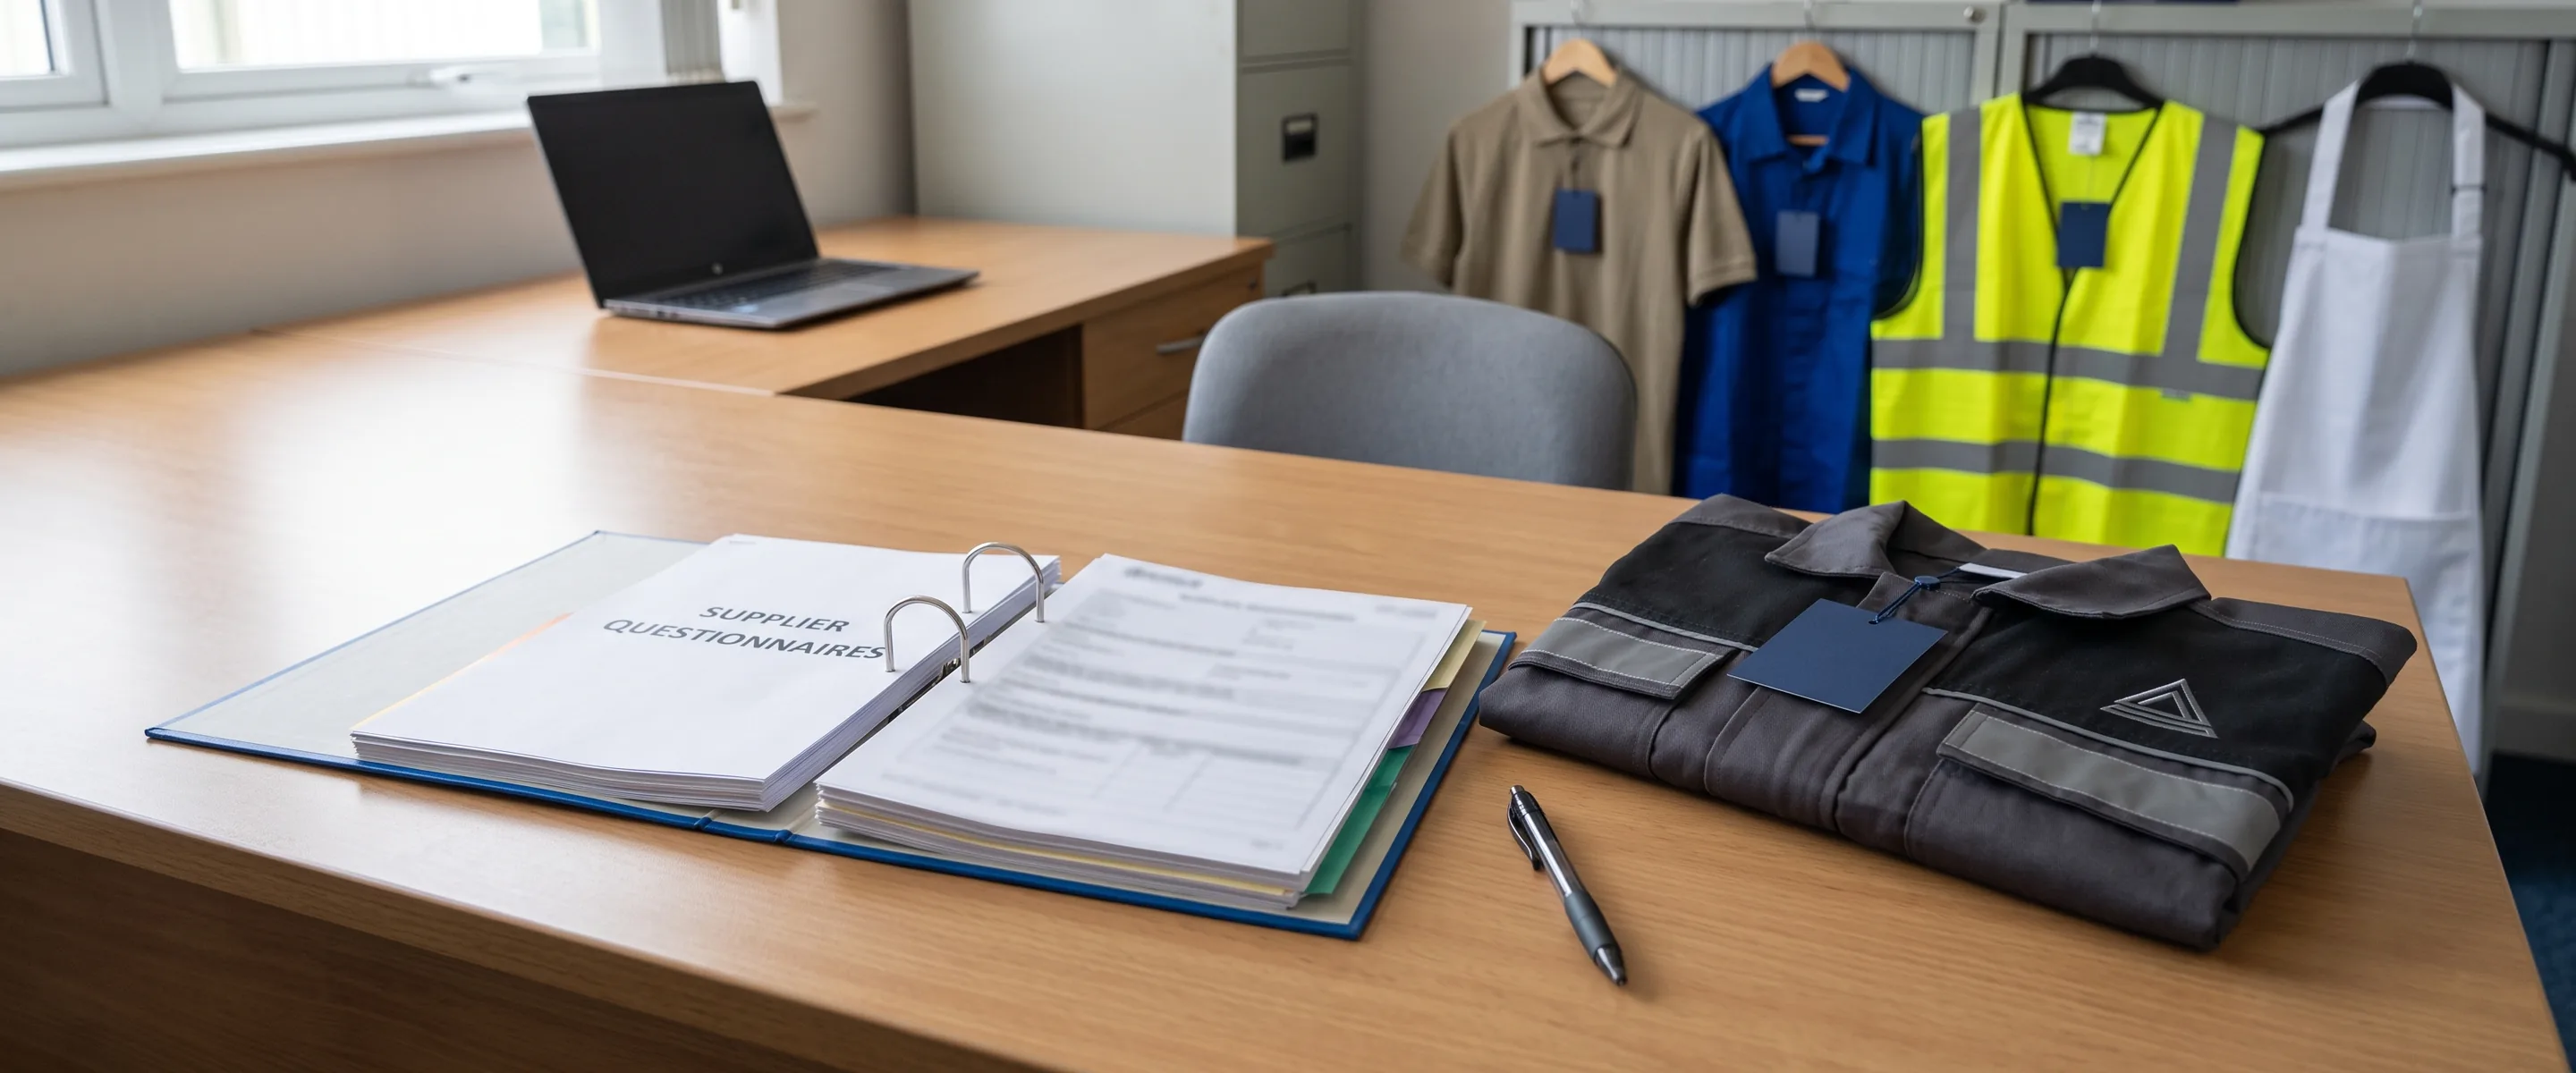
Send Your Supplier Quality Questionnaire

Or your QA manual. It comes back completed within 3 business days, with the QC plan for your program.
Send Your Questionnaire
What comes back
  1. Completed questionnaire
  2. QC plan for your program
  3. Document list for your builds
11Reflective tape

Reflective Tape Wash Test: 50 Industrial Washes on Your Own Fabric

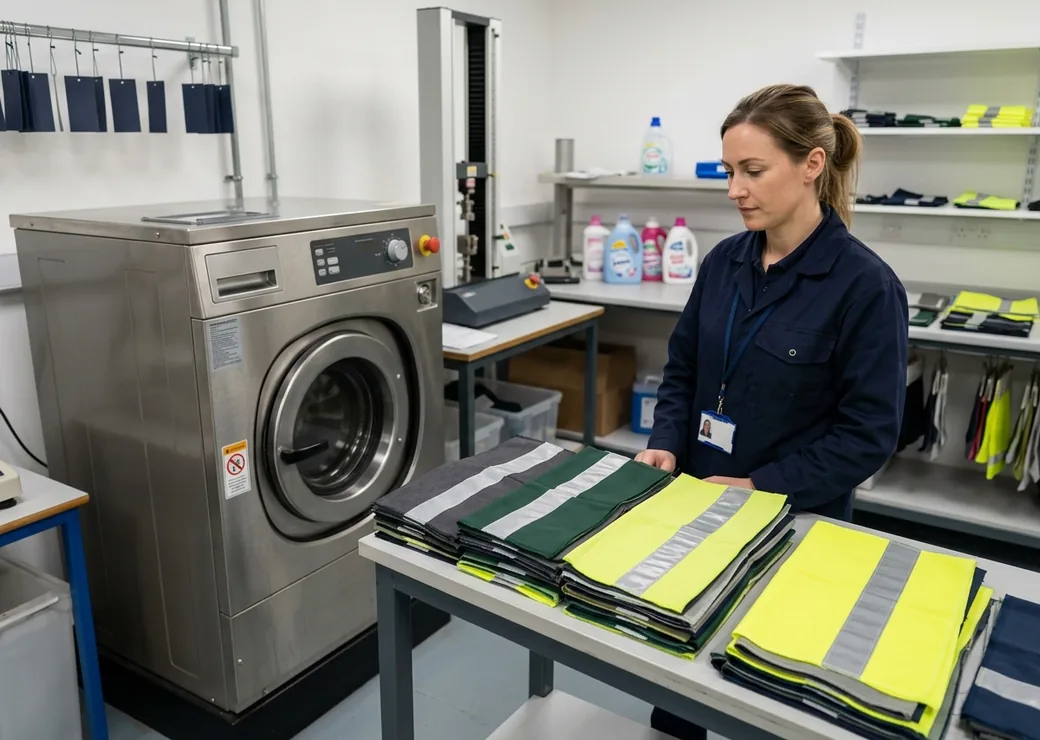
50 is also the maximum wash count on the compliance label of our hi-vis garments. Test pieces are your build: the tape pressed onto your program's own background fabric with the press settings fixed on your first piece.
A test-room washing machine with a stack of fabric pieces carrying reflective tape beside it
Industrial laundering
ISO 15797 × 50
Domestic or commercial
ISO 6330 × 50
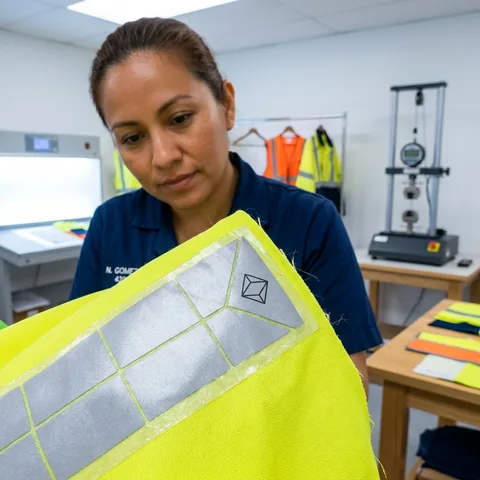
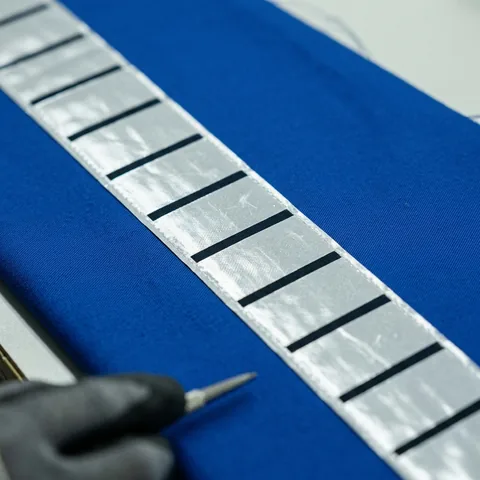
Macro of the corner of a silver reflective tape segment bonded flat
After 50 cycles

No edge lift

Edges and corners of every segment stay bonded flat.
A full run of segmented reflective tape across a fluorescent vest
After 50 cycles

No segment loss

No segment comes away from the fabric.
Close view of the reflective face of the tape, unbroken
After 50 cycles

No cracking

Nothing cracks across the reflective face.
When it runs. On your sample, results sent with it. Industrially laundered programs repeat it on pre-production pieces and bulk leaves only after a pass, inside the 25–35-day bulk window. When it fails. Press settings are adjusted and retested; if it still fails, the tape or method changes, and you hear first.
Tested here
How the tape stays bonded after 50 washes on your fabric and settings.
From the tape mill
Retroreflective performance after washing, taken from the mill's test report for the tape lot on your order. We do not measure retroreflection in-house and make no claim of our own on it.
You receive before and after photos, the test record sheet and the mill report; third-party garment testing is arranged per order on request. Position tolerance and press set-up: custom safety vests.
12Garment tests

Garment, Decoration and Build Tests on Samples and Bulk

Run on samples, pre-production pieces or bulk.
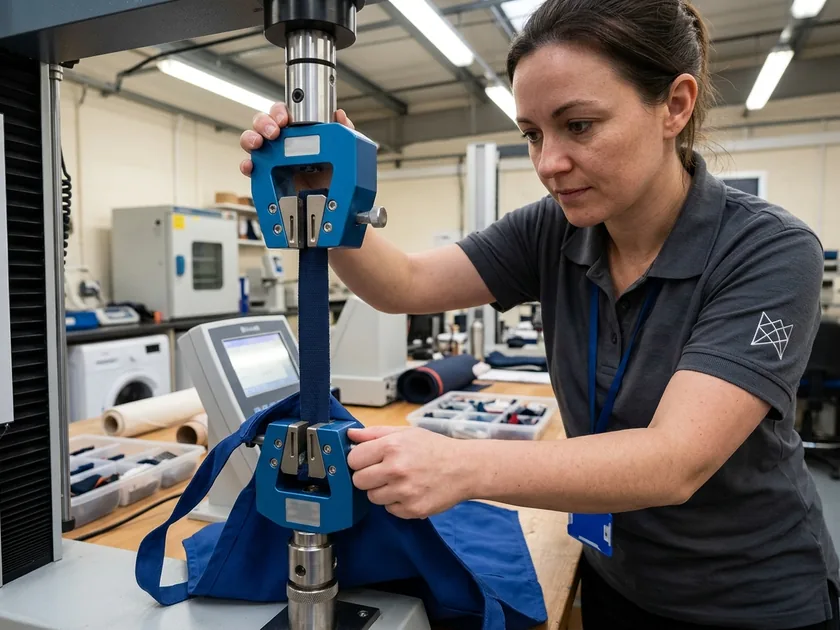
An apron strap clamped in a pull tester while a technician adjusts the grip
Show tests for
Put these tests in my QC plan
Garment, decoration and build tests
TestMethod and pass levelApplies toFull method
Decoration wash testISO 6330 × 50 domestic or ISO 15797 × 50 industrial; no broken stitches, puckering, cracking or edge lift; ISO 105-C06 grade 4 or betterEvery new logo and fabricWork shirts
Reflective tape wash testBond after washing on your own fabric, as set out aboveHi-vis vests, shirts, jackets, coveralls, pantsTape test
Fluid drip testEngine oil, grease, DOT 4 brake fluid and parts-cleaner solvent, 1 h dwell, then one industrial wash; no lift, cracking or bleed, grey scale 4 or betterMechanic uniformsMechanic uniforms
Movement testSquat, kneel, reach and climb in the base and largest size, signed by the pattern room leadCoveralls, work pantsCoverallsWork pants
Strap and hardware pull testStrap joins 150 N held 10 s; grommets, rivets, buttons and snaps 100 N; every sample piece and 3 pieces per bulk lotAprons, chef coatsApronsChef coats
Logo-area checkBackground area left after the logo, calculated on the smallest size on the order against the standard's minimumHi-vis vestsSafety vests
Tape position±5 mm against the build spec sheet, on every sizeHi-vis buildsSafety vests
FR line clearanceLine QC signs that no non-FR thread or trim is left on the line before an FR order startsFR buildsFR clothing
Softshell peel checkLow-temperature transfer pressed at 130–140 °C, checked for edge lift after coolingSoftshell jacketsWork jackets
Decoration first piece and positionFirst piece off every machine and press checked by line QC; ±5 mm against the logo set-up recordEvery decorated garmentEmbroidery and printing
Measurement tolerance±1 cm on coverall and pant length points, ±1.5 cm chest, ±0.5 cm pant riseCoveralls, work pants, work jacketsCoverallsWork pantsWork jackets
Label checkLabel text, position and size label against the garment, inside the final inspectionPrivate label programsPrivate label
Name accuracyEvery name checked at end of line against the signed spelling proofNamed and pack-by-person programsWork shirts
Third-party garment testingArranged per order on requestHi-vis and FR builds, or any program that asksYour inspection
13QC records

QC Records Kept 3 Years After Your Last Delivery

Every check on this page leaves a signed record, kept with your program while it is active and for 3 years after its last delivery.
  • A questioned deliveryThe carton label leads to the dye lot, the lay, the line and that day's records.
  • A re-orderThe previous order's final inspection report is the comparison for the new one.
  • Your accessAsk for any record on your own orders, at any time while it is kept.
Signed inspection sheets filed in a program binder beside a hanging approved sampleProgram-level records and who holds each: about our factory.
3years after your last delivery
Roll inspection sheets, shade readings, trim lot checks, FR trim records, mill test reports
Cut-panel check sheets for every lay
First-piece approvals, roving check sheets, line-clearance records
End-of-line check sheets and daily measurement records
Decoration and tape wash tests with photos; movement and pull tests
Hold tags, repair and remake decisions, the signed final inspection report
14Document pack

QC Document Pack: The Reports That Come With Each Order

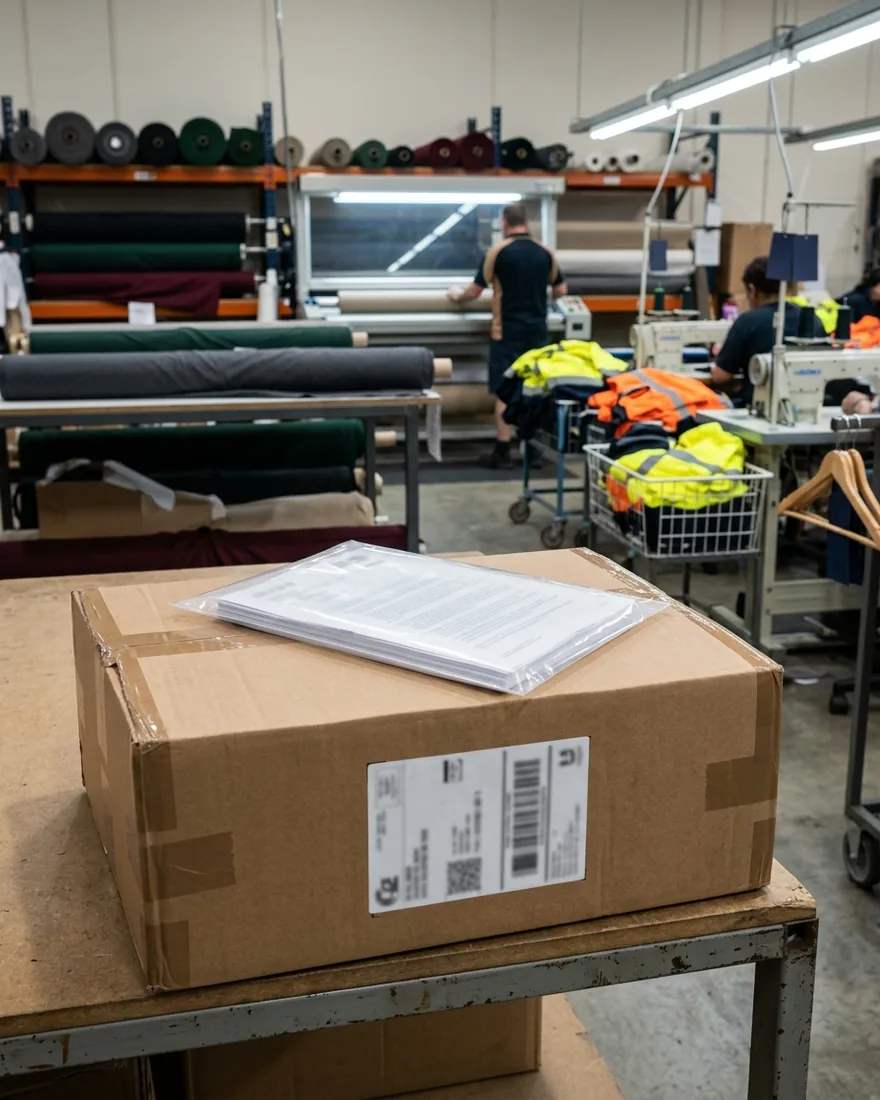
What you receive depends on the build. The final inspection report comes with every order.
A document pack in a clear sleeve lying on a labelled carton
  • Every order

    Final inspection report

    With photos and the QC manager's signature, before the goods leave.
  • Decorated

    Decoration wash test record

    Before and after photos and the test sheet for each logo and fabric.
  • Hi-vis

    Reflective tape wash test record

    Photos, test sheet and the tape mill's report.
  • Hi-vis · FR

    Mill test reports

    For every fabric and tape lot on the order.
  • Hi-vis · FR

    Signed build spec sheet

    Per style, with the per-size area table on hi-vis vests.
  • FR

    FR document pack

    Signed FR BOM, line-clearance record and component reports. FR clothing
  • As needed

    Product test records

    Movement, pull or fluid drip tests where the garment calls for them.
  • Every order

    Carton list

    PO, style, colour and dye lot; employee name, size and site for pack-by-person orders.
  • On request

    Third-party garment test report

    When arranged for your order.
amfori BSCI audit summary and OEKO-TEX Standard 100 fabric certificates on request; which approval each answers is on our home page.Send your approval checklist
A buyer's QA inspector and our final inspector checking a garment side by side, with the approved sample and size chart on the table
A third-party inspector measuring a polo with a tape measure
A laptop camera pointed at the final inspection tableLive video
You pick the cartons
15Your inspection

Buyer and Third-Party Inspection at Our Final Inspection Table

  • Your QA or your agency

    Welcome at the final inspection of your order. We notify the date 3 business days ahead, and your inspector works beside ours with the approved sample, build spec and measurement spec on the table.
  • Live video

    If you cannot send anyone, the final inspection runs on a live call. You choose which cartons are opened and which pieces are measured.
  • The report either way

    Sent before the goods leave, whether or not you attend.
  • Your own level

    A stricter AQL or extra checks: tell us at quote stage, and both inspectors work to that plan.
Third-party garment testing is arranged per order on request and built into the sample plan.Factory visits and video walk-throughs before you order: about our factory.
Book your inspector for final inspection
Your QC plan

Start Your Uniform Program With a QC Plan

Send your garments, standard and wash route. A written quote comes back within 1 business day, with the inspection and test plan for your program.
What to send
  • Garments and quantities
  • Hi-vis or FR standard
  • Wash route
  • Decoration
  • Inspection level
  • Tests you require
  • Documents you need
  • Your questionnaire
  • Inspection attendance
  • A written quote
  • An inspection and test plan
  • A document list for your builds
Prefer another channel? Contact page
A packer sealing a carton after final inspection, carton label facing out
Please enter your name.
Please enter your company.
Please enter a valid email.
Garments
Wash route
Inspection level
Inspection attendance
Questionnaire, QA manual or approval checklist: email it to [email protected].